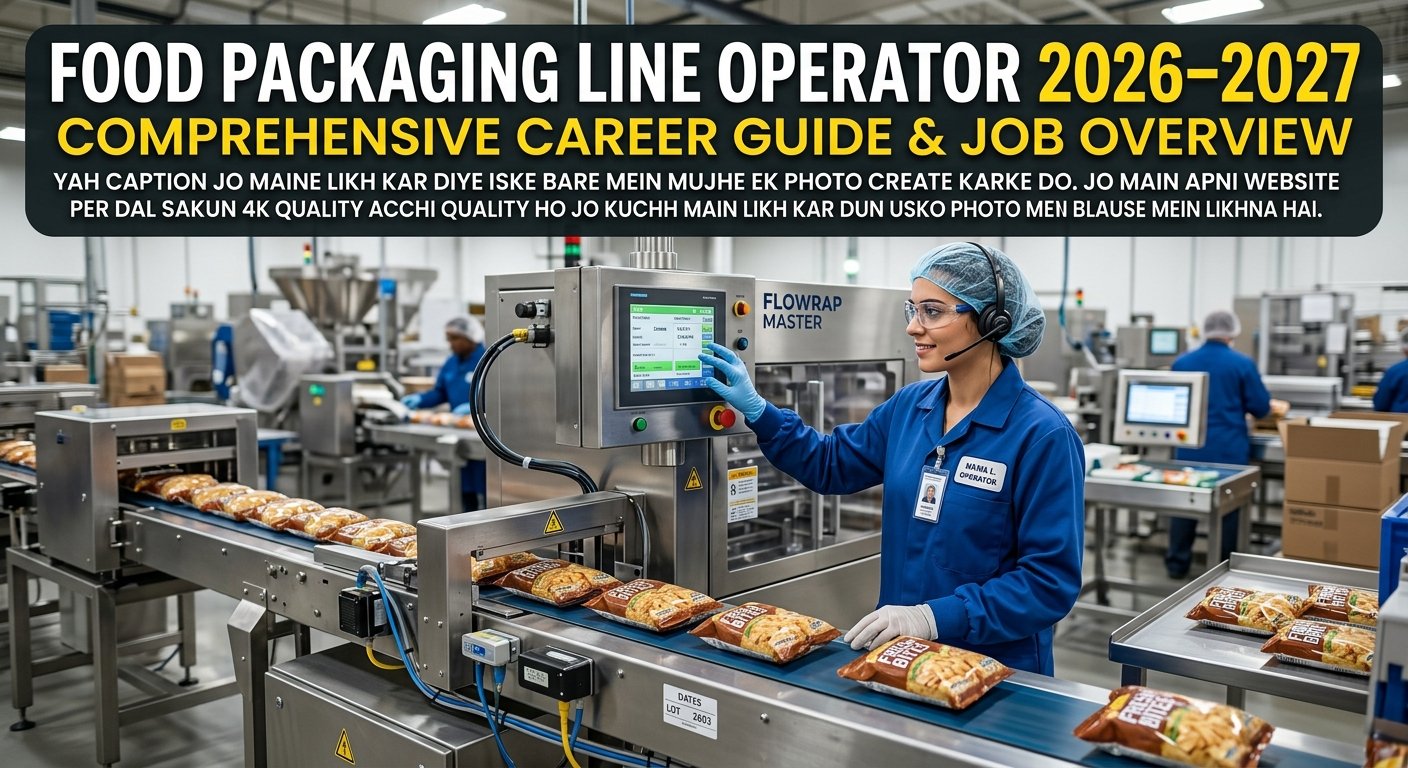
The modern food processing and manufacturing industry relies heavily on automation, precision, and strict safety protocols. At the heart of this supply chain is the Food Packaging Line Operator, a critical role that ensures consumable goods move safely from production facilities to store shelves worldwide.
As consumer demand for packaged, ready-to-eat, and eco-friendly food products increases, the job market for packaging line operators remains strong. Below is an in-depth breakdown of the responsibilities, required skills, work environment, and career trajectory for a Food Packaging Line Operator.
Key Responsibilities of a Food Packaging Line Operator
Food Packaging Line Operators oversee, manage, and troubleshoot automated machinery involved in sealing, labeling, wrapping, and boxing food items.
- Machinery Setup & Operation: Calibrating, starting, and monitoring conveyor systems, flow wrappers, automated sealers, weight checkers, and industrial labeling equipment.
- Quality Control (QC): Inspecting finished packages to ensure airtight seals, correct weight measurements, clear expiration dates, and error-free labeling.
- Material Management: Loading raw packaging supplies—such as plastic films, cardboard boxes, trays, and aluminum foils—into high-speed machinery.
- Hygiene and Sanitization: Enforcing strict Good Manufacturing Practices (GMP), Hazard Analysis Critical Control Point (HACCP) standards, and food safety protocols.
- Basic Maintenance & Troubleshooting: Clearing line jams, resetting machine parameters, and performing routine preventive maintenance to prevent costly production downtime.
Technical Skills & Qualifications
While many entry-level packaging positions provide on-the-job training, candidates with specific technical aptitudes stand out during hiring processes:
| Category | Key Requirements |
| Education | High School Diploma or equivalent (vocational/technical certifications preferred). |
| Technical Aptitude | Understanding of automated conveyance, pneumatic systems, sensors, and basic mechanical troubleshooting. |
| Regulatory Knowledge | Familiarity with Food and Drug Administration (FDA) rules, GMP standards, and OSHA workplace safety regulations. |
| Physical Stamina | Ability to stand for long shifts, lift heavy packaging materials (up to 50 lbs), and handle repetitive motions. |
| Attention to Detail | Sharp eye for spotting misaligned labels, damaged packaging, or compromised seals instantly. |
Work Environment and Shift Expectations
Food manufacturing plants operate around the clock to meet global food supply demands. Packaging operators typically work in fast-paced factory environments. Key work conditions include:
- Shift Work: Options for 8-hour or 12-hour shifts, including night, weekend, and rotating schedules.
- Temperature Variations: Working in temperature-controlled environments, which may range from climate-controlled dry plants to cold storage/refrigerated processing facilities.
- Safety Gear Requirements: Standard wear includes hairnets, ear protection, non-slip steel-toe boots, protective gloves, and hi-vis safety vests.
Career Growth & Salary Expectations (2026–2027)
Starting as a Food Packaging Line Operator opens doors to several advancement pathways within industrial manufacturing:
- Entry-Level Packaging Operator: Focuses on line loading, monitoring, basic checks, and packing.
- Senior Packaging Technician: Manages complex machine setups, automated changeovers, and advanced line diagnostics.
- Packaging Line Lead / Shift Supervisor: Oversees entire production shifts, manages team workflows, and enforces safety compliance.
- Maintenance Mechanic / Quality Assurance Inspector: Moves into dedicated technical repair or specialized quality assurance departments.